A practical manufacturing partner
for demanding mold work.
Huicheng combines precision machining, EDM, wire cutting, grinding, inspection and mold trials in one coordinated Dongguan operation.
Built around
process control.
Dongguan Huicheng Precision Mold Co., Ltd. operates from Chang’an, Dongguan—one of China’s established mold-manufacturing clusters. Founded in September 2010, the company has 16 years of precision machining experience, an approximately 1,500 m² facility and a team of around 30 people.
Precision plastic mold components are the core business. Complete injection molds, carrier-tape and precision stamping tooling, mold trials and project-specific injection support extend the same drawing-led workflow. Work includes connector mold components, automotive electronics inserts and precision stamping die parts.
No outsourced critical processes
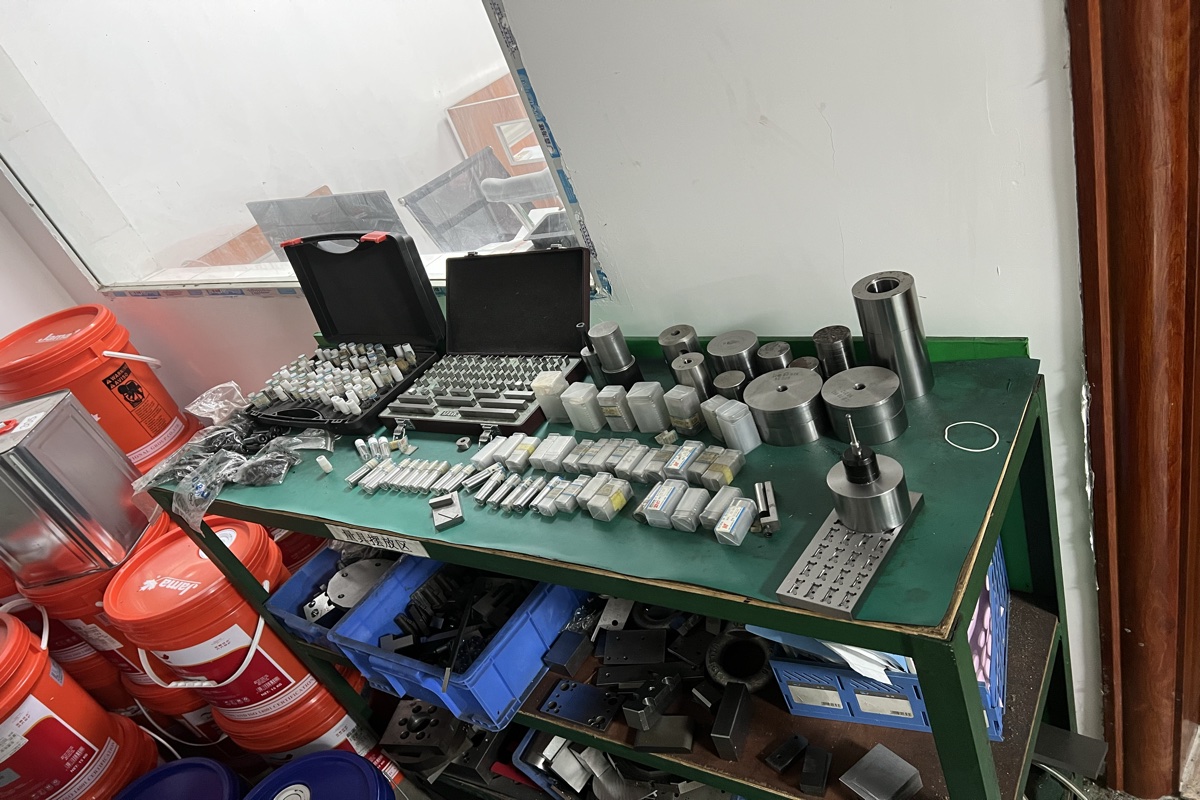
CNC, electrode machining, EDM, slow-wire cutting, precision grinding and CMM inspection are all kept in-house—so delivery and quality are not dependent on a subcontractor’s schedule.
Measurement reports when you need them
IQC, PQC and FQC checkpoints are backed by CMM, 2.5D vision, projection and hardness measurement. Dimensional inspection reports and hardness certificates are available per project on request.
Material traceability and ISO 9001
Huicheng operates under ISO 9001. Material certificates and post-heat-treatment hardness records are retained for every project. Stock material is verified before machining begins.
Purpose-built
for demanding tolerances.
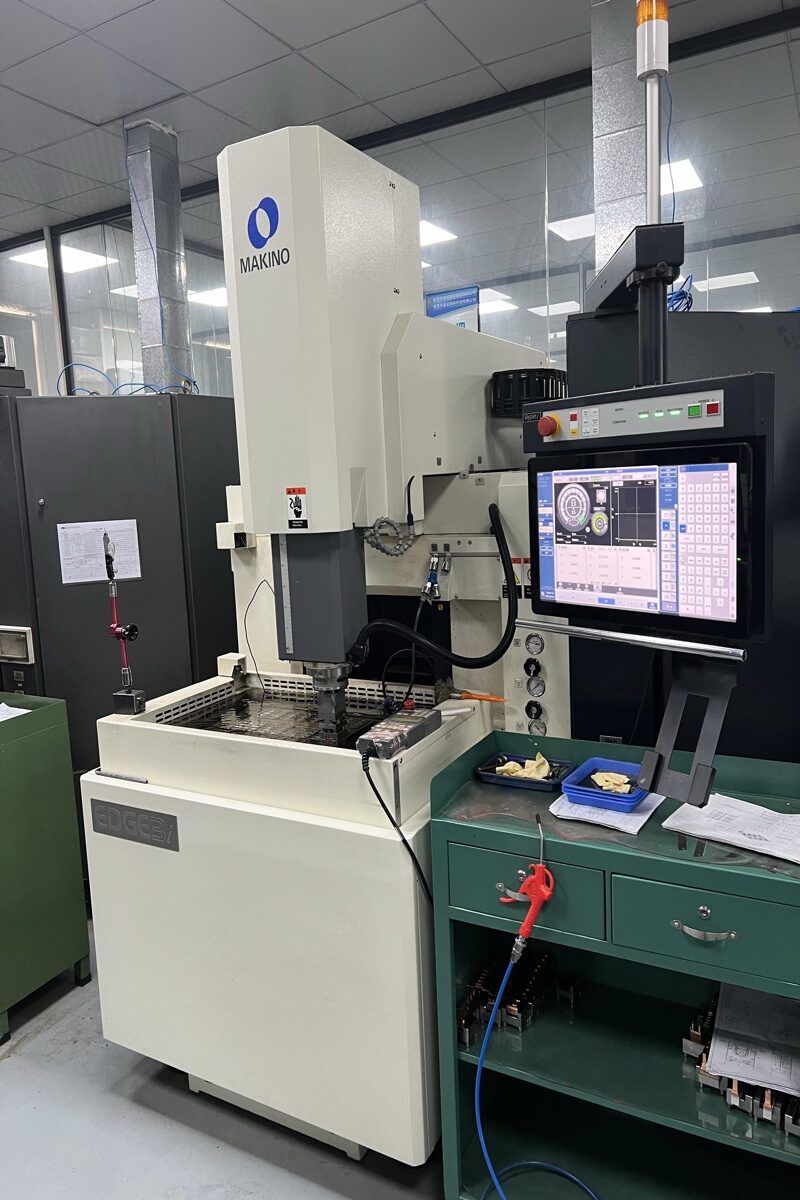
Makino EDGE3 — Sinker EDM
High-accuracy die-sinking EDM for complex cavity and electrode work requiring tight surface finish and tight positional tolerances.
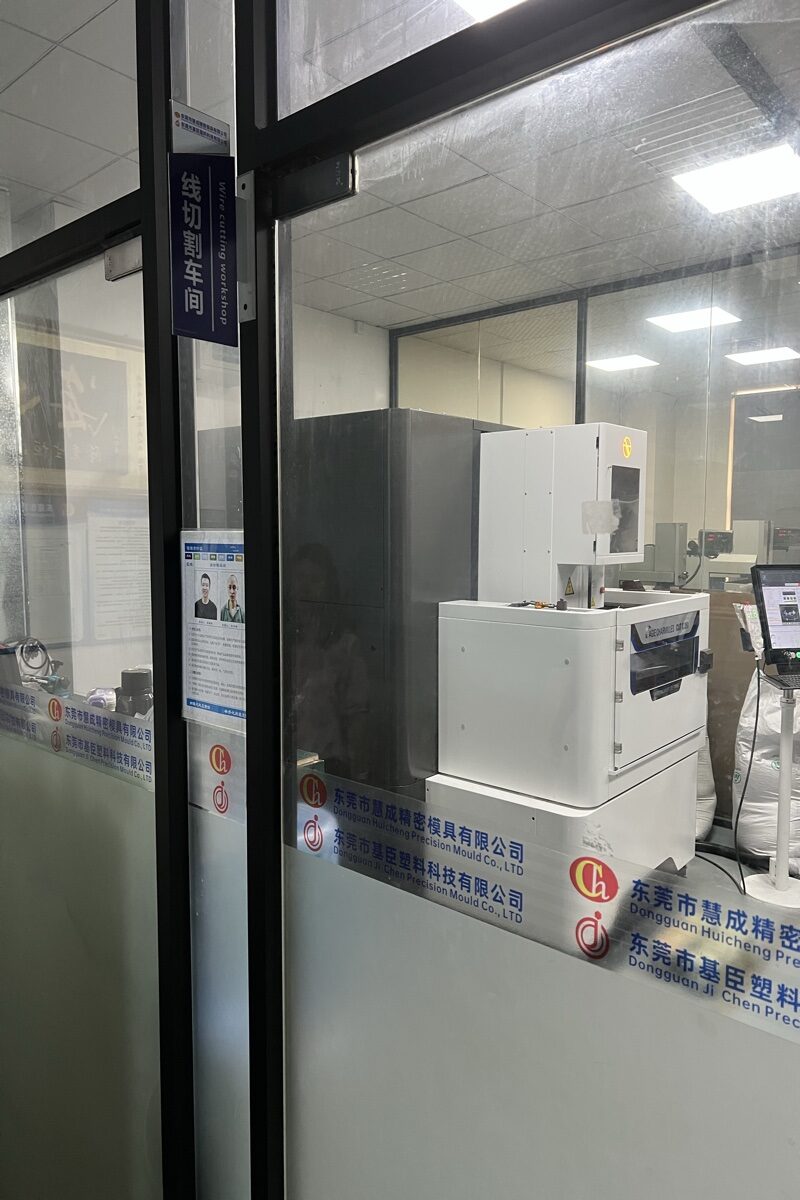
AGIE CHARMILLES CUT C 350 — Slow-Wire EDM ×2
Swiss slow-wire cutting system for precision profiles, punches and inserts with high surface quality and dimensional repeatability. Ra 0.3 achievable.
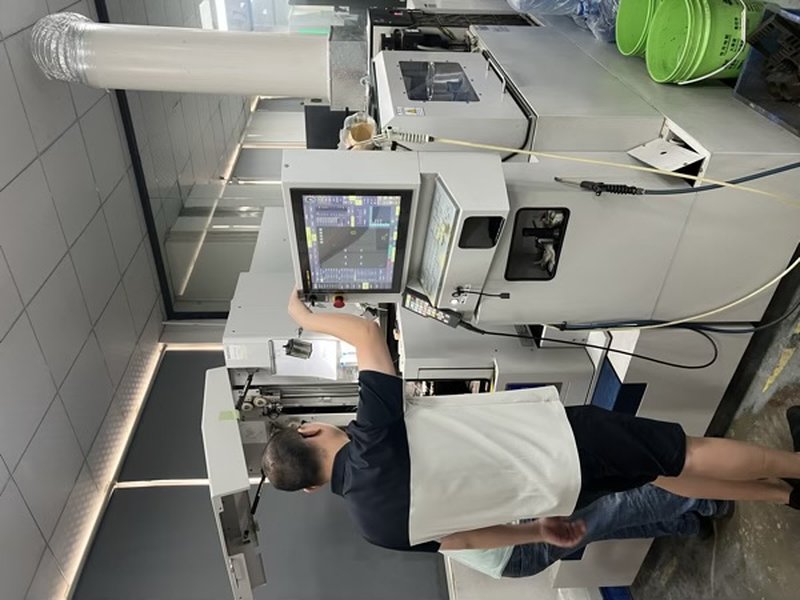
Seibu M50B / M35B — Slow-Wire EDM ×2
Japanese slow-wire EDM machines for fine-feature wire cutting work. Together with the AGIE fleet, four dedicated slow-wire machines cover a wide range of profile, punch and insert geometries.
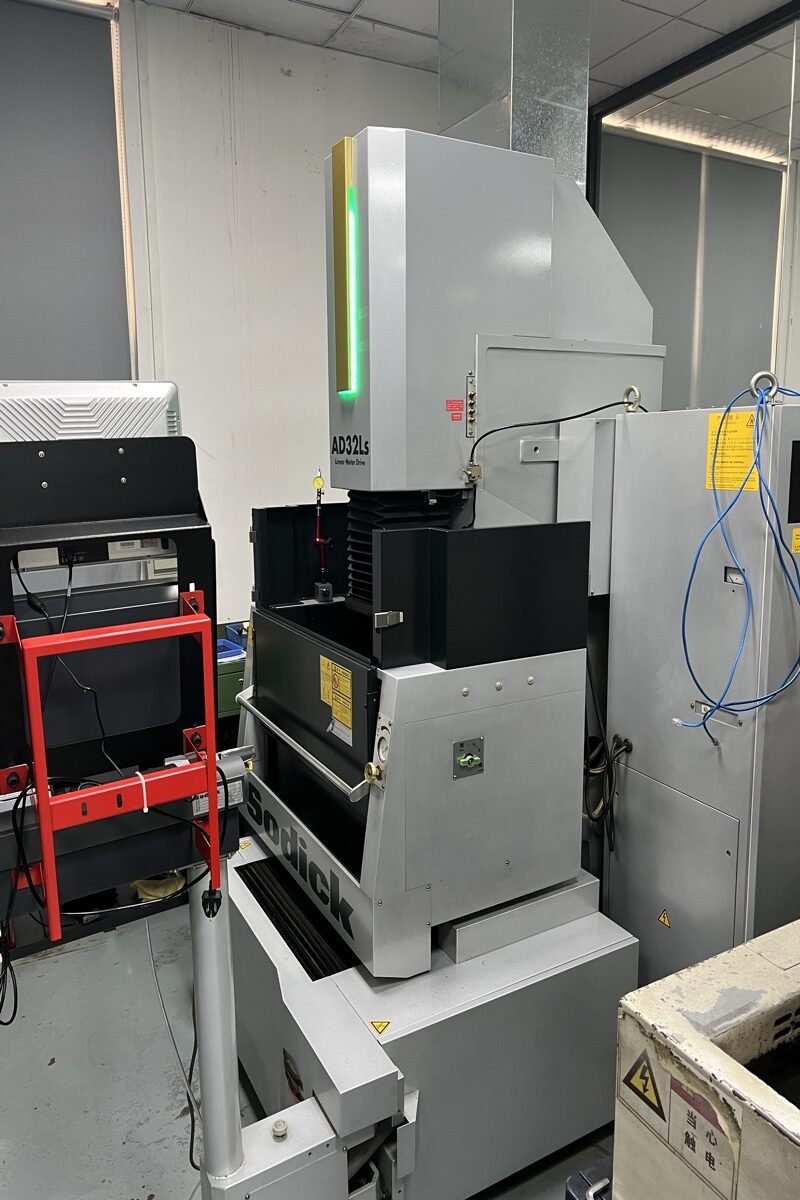
Sodick AD32Ls — Linear Drive EDM
Japanese linear-motor sinker EDM for demanding accuracy on small cores, slides and connector-type cavities.
DAHLIH MCV-860 — CNC Machining
Vertical machining center for mold base work, cavity roughing, electrode blanks and contoured surfaces.
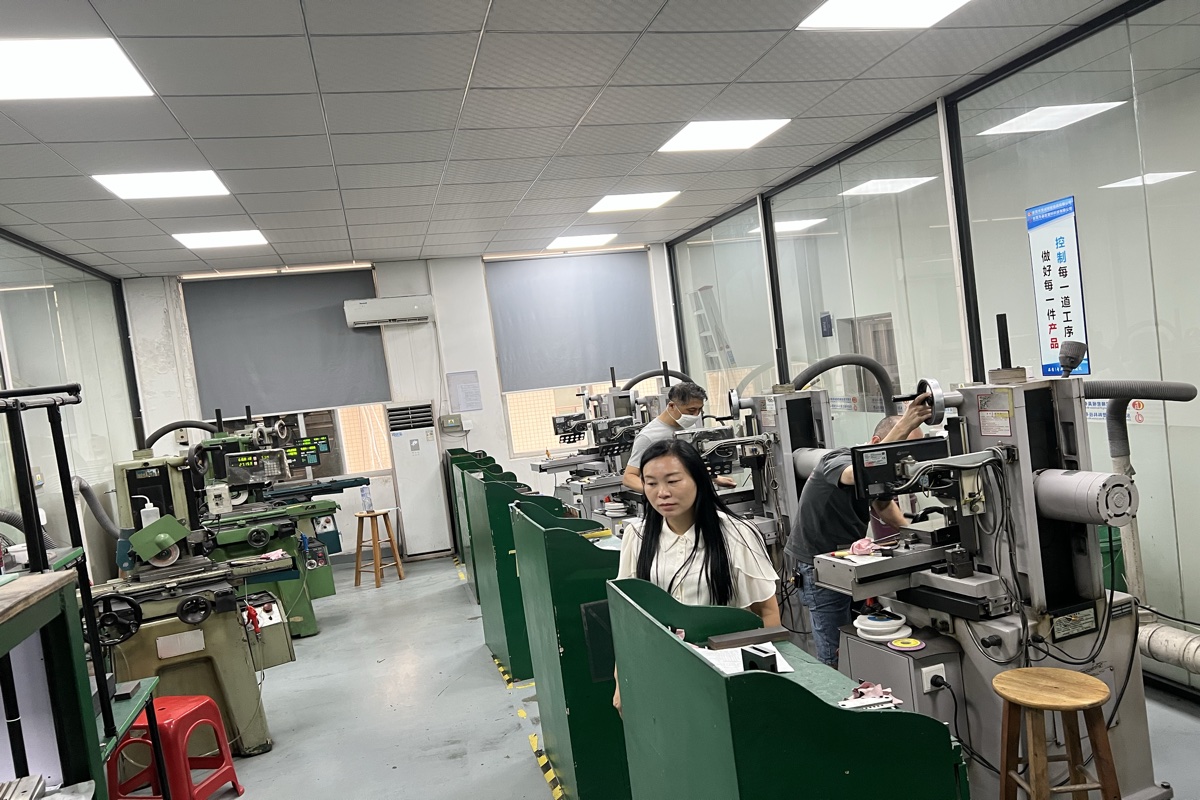
Precision Grinding
Surface and profile grinding for mold inserts, cores and flat reference surfaces; essential for meeting tight thickness and flatness requirements.
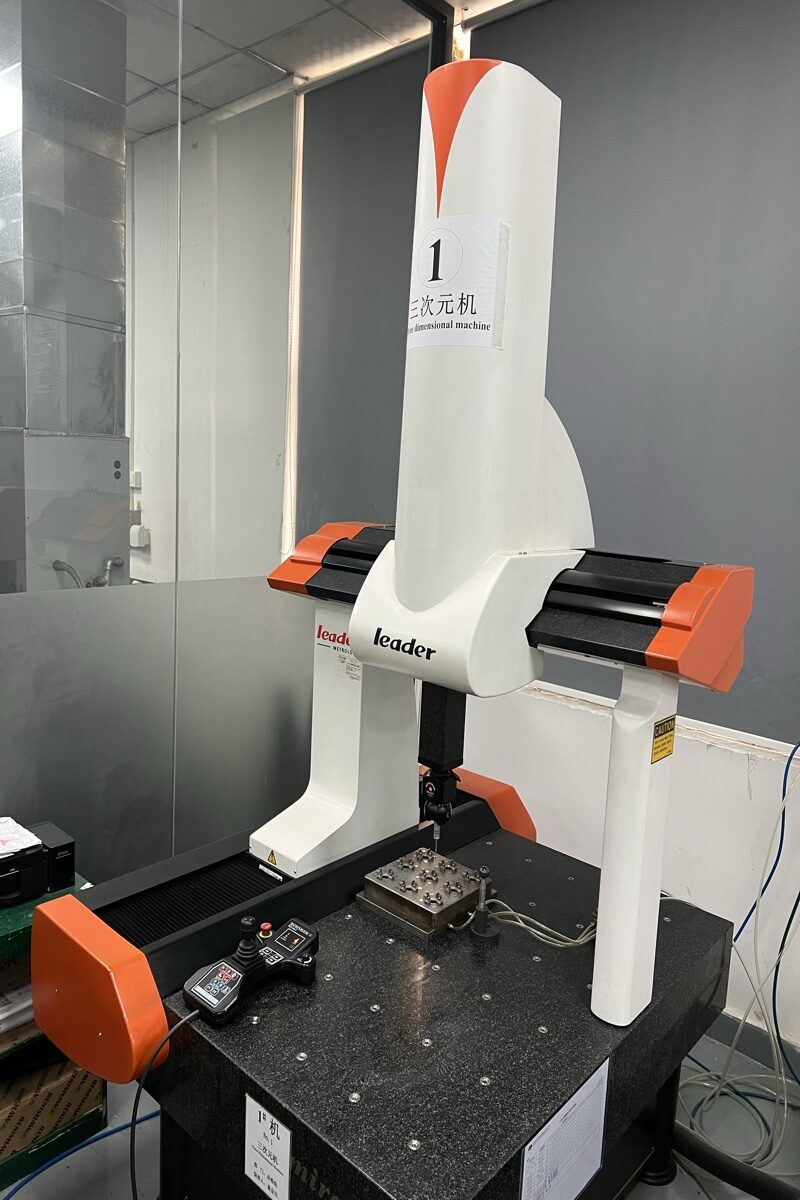
CMM & 2.5D Vision Inspection
Coordinate measuring machine and 2.5D optical measurement for dimensional verification and final inspection reporting.

One drawing.
One coordinated plan.
Material sourcing, rough and finish machining, electrode work, EDM, wire cutting, grinding and inspection are coordinated against the same drawing and delivery target.
Industries and applications
we regularly supply.
Connector components · Automotive electronics · Consumer electronics · Precision stamping dies · Medical aesthetics
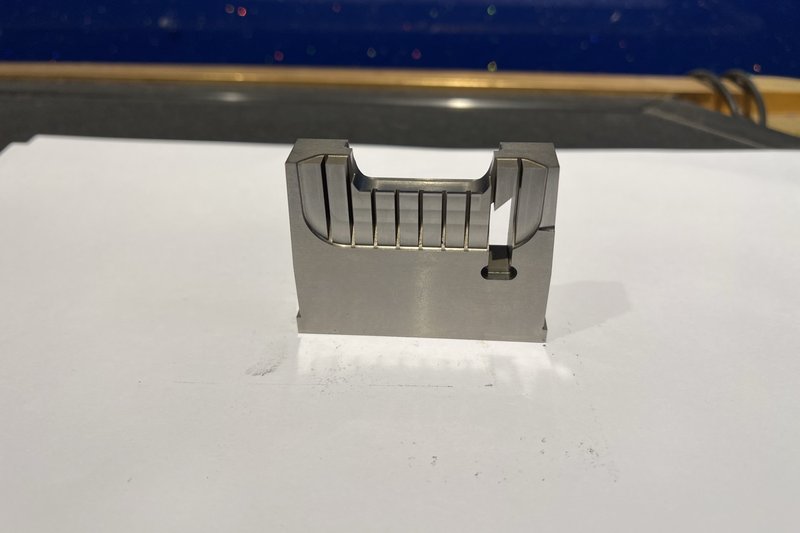
Multi-slot connector mold insert
Challenge: Eight parallel EDM slots at equal pitch, thin walls between slots, curved assembly pocket and multiple locating holes — all holding position and form within drawing tolerance.
Process: CNC roughing → slow-wire EDM (slot profiles) → surface grinding → 2.5D vision + CMM inspection.
Result: Slot pitch within ±0.01 mm across all positions; Ra 0.3 on critical surfaces; full CMM report delivered with parts.
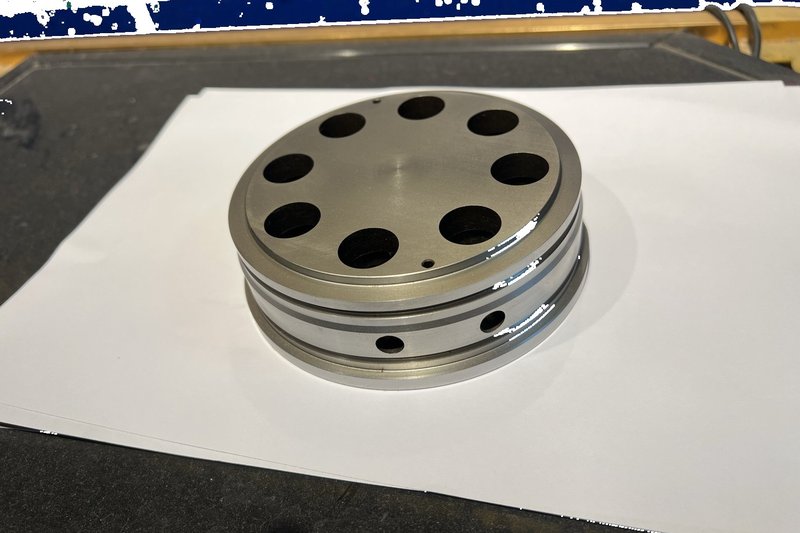
Circular mold plate with symmetrical hole pattern
Challenge: Eight symmetrically distributed through-holes on a circular pattern, stepped OD concentricity, side radial holes intersecting the main body — total runout control across all features.
Process: CNC turning and milling → OD and face grinding → CMM dimensional verification at multiple datums.
Result: Hole position tolerance and concentricity confirmed by CMM; inspection report issued with delivery.
Carrier tape punching die components
Challenge: Punch pitch must match carrier tape perforation standard across the full die width; cutting edges must be consistent and interchangeable for field replacement without re-adjustment.
Process: CNC → slow-wire EDM (punch profiles and die openings) → surface grinding → hardness verification (HRC58+) → assembly trial.
Result: Pitch dimensions consistent across all punches; components replaceable individually; hardness and dimensional records retained per project.
Buyer questions. Answered directly.
Send your drawing.
Share your 2D/3D file and requirements. We’ll identify the process route, flag any DFM concerns, and return a clear quotation with the technical questions that need answering.